
How Bulk Drug Intermediates Enhance Drug Formulation Efficiency
Jun 29,2026


How Bulk Drug Intermediates Enhance Drug Formulation Efficiency
Table of Contents
1. Introduction to Bulk Drug Intermediates
2. Understanding Drug Formulation
3. The Role of Bulk Drug Intermediates in Drug Development
3.1 Definition and Importance
3.2 Types of Drug Intermediates
3.3 Regulatory Considerations
4. Enhancing Drug Formulation Efficiency
4.1 Streamlining the Production Process
4.2 Cost-Effectiveness and Resource Optimization
4.3 Quality Assurance and Control
5. Case Studies: Successful Applications of Bulk Drug Intermediates
6. Future Trends in Bulk Drug Intermediates
7. FAQs about Bulk Drug Intermediates
8. Conclusion
1. Introduction to Bulk Drug Intermediates
In the fast-evolving pharmaceutical industry, bulk drug intermediates serve as crucial components in the drug formulation process. These intermediates act as building blocks for active pharmaceutical ingredients (APIs), facilitating more efficient and streamlined production of various medications. By understanding how these intermediates function, we can appreciate their significance in enhancing drug formulation efficiency.
2. Understanding Drug Formulation
Drug formulation involves designing a specific composition of pharmaceutical ingredients to produce a safe and effective medication. The formulation process encompasses several stages, including the selection of raw materials, the development of the drug delivery system, and thorough testing to ensure product quality and efficacy. It is a complex and time-consuming process, which is why the role of bulk drug intermediates cannot be overstated.
3. The Role of Bulk Drug Intermediates in Drug Development
3.1 Definition and Importance
Bulk drug intermediates are chemical compounds that serve as precursors in the production of APIs. These intermediates are essential as they ensure that the final drug product meets the required quality standards while maintaining cost-effectiveness. By utilizing intermediates, manufacturers can optimize their processes and enhance the overall efficiency of drug development.
3.2 Types of Drug Intermediates
Various types of bulk drug intermediates exist, each serving a unique purpose in the drug formulation process. Common categories include:
- **Chiral Intermediates**: These are essential for creating enantiomerically pure APIs, which are crucial for the efficacy and safety of certain medications.
- **Prodrug Intermediates**: These are inactive compounds that metabolize into active drugs within the body, improving bioavailability and therapeutic effects.
- **Building Blocks**: Simple compounds that serve as the foundation for synthesizing more complex pharmaceutical agents.
3.3 Regulatory Considerations
The production and use of bulk drug intermediates are subject to stringent regulatory standards. Regulatory bodies like the FDA and EMA impose guidelines to ensure safety, efficacy, and quality. Compliance with these regulations is vital for manufacturers looking to maintain their market position and build trust with healthcare providers and patients.
4. Enhancing Drug Formulation Efficiency
Bulk drug intermediates significantly contribute to the efficiency of drug formulations through several mechanisms.
4.1 Streamlining the Production Process
By incorporating bulk drug intermediates into the manufacturing process, pharmaceutical companies can simplify complex synthesis pathways. This streamlining reduces the number of steps required to produce an API, ultimately shortening development timelines. For example, using a specific intermediate can eliminate the need for certain reactions, thus accelerating the overall production process.
4.2 Cost-Effectiveness and Resource Optimization
The utilization of bulk drug intermediates also leads to cost savings in drug formulation. Producing intermediates in bulk allows manufacturers to take advantage of economies of scale, reducing per-unit costs. Furthermore, optimally designed intermediates can minimize waste and resource consumption, contributing to a more sustainable manufacturing process. This is particularly important as the pharmaceutical industry faces increasing pressure to reduce operational costs without compromising quality.
4.3 Quality Assurance and Control
Incorporating bulk drug intermediates can enhance the quality of finished pharmaceutical products. Quality assurance processes can be streamlined by monitoring the quality of intermediates at various stages of production. By ensuring that intermediates meet specific quality standards, manufacturers can reduce the likelihood of defects in the final product, thereby improving patient safety and therapeutic outcomes.
5. Case Studies: Successful Applications of Bulk Drug Intermediates
Real-world examples demonstrate the effectiveness of bulk drug intermediates in enhancing drug formulation efficiency. For instance, a leading pharmaceutical company successfully utilized a chiral intermediate to develop a new antipsychotic medication. By employing this intermediate, they not only accelerated the development process but also improved the drug's safety profile, leading to a successful market launch.
Another case involved a biopharmaceutical firm that leveraged prodrug intermediates to enhance the bioavailability of a critical cancer treatment. By reformulating the drug using these intermediates, they achieved a significant increase in patient response rates, highlighting the impact of intermediates on therapeutic efficacy.
6. Future Trends in Bulk Drug Intermediates
The future of bulk drug intermediates is promising, driven by advancements in technology and growing demand for innovative therapeutics. Trends to watch include:
- **AI and Automation**: The integration of artificial intelligence and automation in drug development will allow for more precise and efficient production of bulk drug intermediates.
- **Sustainability Practices**: As the pharmaceutical industry shifts toward more sustainable practices, the development of greener intermediates and processes will become increasingly important.
- **Personalized Medicine**: The rise of personalized medicine will drive the need for tailored intermediates that cater to specific patient profiles, enhancing treatment efficacy.
7. FAQs about Bulk Drug Intermediates
7.1 What are bulk drug intermediates?
Bulk drug intermediates are chemical compounds that serve as precursors for active pharmaceutical ingredients (APIs) in drug formulation.
7.2 Why are bulk drug intermediates important in drug manufacturing?
They optimize the production process, enhance cost-effectiveness, and improve product quality, all of which are essential for successful drug development.
7.3 How do regulatory standards impact bulk drug intermediates?
Regulatory standards ensure that bulk drug intermediates meet safety and quality criteria, affecting their production and use in pharmaceuticals.
7.4 Can bulk drug intermediates reduce drug formulation costs?
Yes, by enabling economies of scale and minimizing waste, bulk drug intermediates can lead to significant cost savings in drug formulation.
7.5 What is the future of bulk drug intermediates in the pharmaceutical industry?
The future includes advancements in AI, sustainability practices, and developments in personalized medicine, which will drive innovation in bulk drug intermediates.
8. Conclusion
In conclusion, bulk drug intermediates play a vital role in enhancing drug formulation efficiency within the pharmaceutical industry. By streamlining production processes, optimizing costs, and assuring quality, these intermediates facilitate the development of effective and safe medications. As technological advancements continue to shape the industry, the importance of bulk drug intermediates will only grow, paving the way for more innovative and efficient drug formulations. Embracing these components is essential for pharmaceutical companies looking to remain competitive and meet the evolving needs of healthcare providers and patients.
Syntame Exhibition Tour 2026

CPHI China 2026 Concludes Successfully | Shentai Bio Will Continue to Focus on High-Content Pharmaceutical Raw Material Solutions
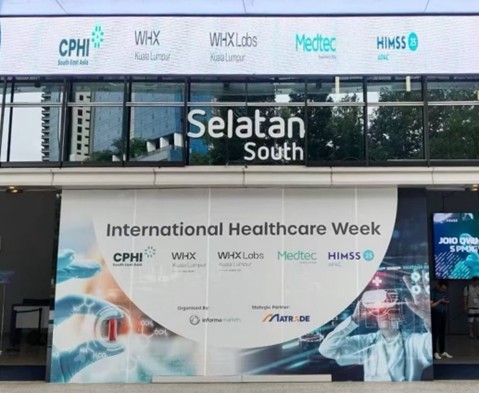
CPHI South East Asia 2025 comes to a successful conclusion | SYNTAME opens a new chapter in the Southeast Asian market
CPHI South East Asia 2025 comes to a successful conclusion | SYNTAME opens a new chapter in the Southeast Asian market
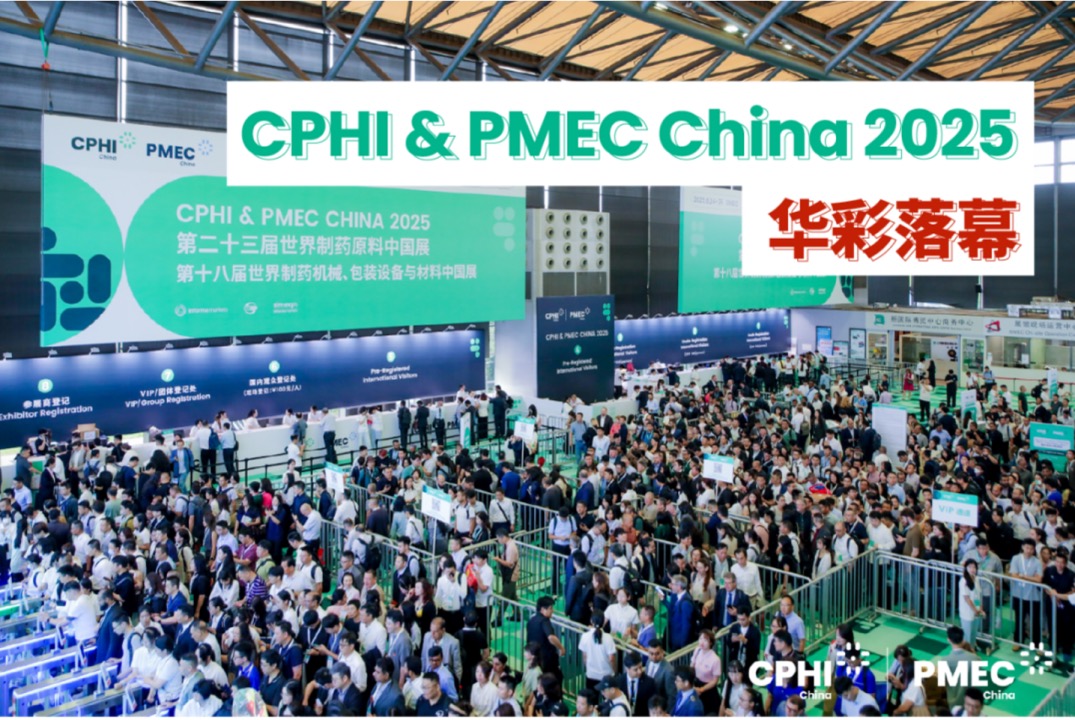
CPHI China 2025 ended successfully | Syntame talks with customers around the world about new opportunities for cooperation
CPHI China 2025 ended successfully | Syntame talks with customers around the world about new opportunities for cooperation
The company team made a stunning appearance at the 22nd World Pharmaceutical Raw Materials China Exhibition (CPHI) at the Shanghai New International Expo Centre.
No.298 Mingguang Road, Urban Industrial Park, Yinzhou District, Ningbo City, Zhejiang Province, P.R. China